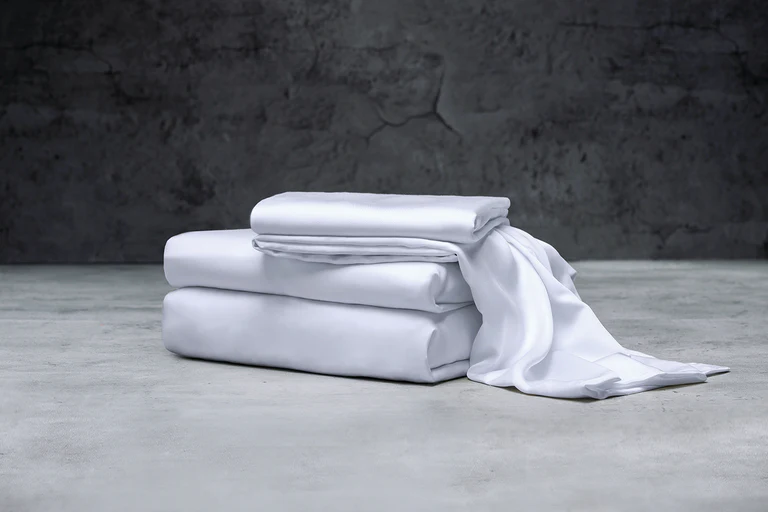
Every sourcing manager has lived this story. A new bedding program launches, the calendar is tight, and someone suggests skipping a sample round to save two weeks. The bulk shipment arrives, the duvet cover is two inches short, the print shade drifted, and the “saved” two weeks become a six-week air-freight rescue plus a discount to keep the retailer quiet. The sample stage that got skipped is always cheaper than the mistake it would have caught.
Developing a bedding program with a factory is not a single handshake; it is a staged conversation where each sample answers one question and locks one answer. This playbook maps the full path from your tech pack to bulk production — proto sample, strike-off, pre-production sample — and the approval discipline that keeps both sides honest. It is written for brand owners, private-label developers, and sourcing teams who want their bedding manufacturers to produce exactly what was approved, nothing more and nothing less.
Why Rushing Development Always Costs More Than It Saves
A bedding set looks simple next to a tailored jacket, but it carries a surprising number of decisions: construction, yarn count, बुनाई, चौडाइ, color standards, print repeats, seam types, closure hardware, elastic specifications, label placement, प्याकेजिङ. Each decision made verbally and remembered differently by two people is a future dispute. The sample stages exist to convert every one of those decisions from words into a physical object both sides can hold.
The economics are unforgiving. A proto sample costs a few dozen dollars and a week. A strike-off costs a little more. A container of wrong goods costs the goods, the freight, the lost season, and sometimes the retail relationship. Professional buyers treat sampling as the cheapest insurance in the program, not as a delay to be minimized. When a factory pressures you to “just go to bulk,” that is information about the factory, not about your timeline.
The Tech Pack: The One Language Both Sides Speak
Everything starts with the tech pack — the document set that describes your product completely enough that a stranger could make it. A serious bedding tech pack includes flat sketches of every piece with callouts, a bill of materials naming each fabric and trim, finished measurements in a graded spec chart, construction details for seams and hems, color references with Pantone TCX codes, artwork files with repeat sizes for prints, label and packaging instructions, and your target price with the quantity tiers behind it.
Two rules make tech packs work. पहिले, numbers beat adjectives: “soft hand feel” means nothing on a costing desk, जबकि “कपास वर्षा, 40s by 40s, 300 थ्रेड गणना, silicone softener” can be priced in an hour. दोस्रो, one document rules them all: every sample and every bulk lot is judged against the latest approved revision, never against an email thread. मा Nantong अखंडता कपडा, the merchandiser converts your tech pack into an internal work order and flags every ambiguity before development starts — because a question answered in week one is free, and the same question in week eight is a claim.
Stage One: The Proto Sample, Proving the Construction
The proto — short for prototype — is the first physical answer to your tech pack. It is usually made in a substitute fabric close to your specification, because its job is not color or hand feel. Its job is construction: do the pieces measure what the spec chart says, do the seams and hems match the drawings, does the fitted sheet pocket depth fit a real mattress, does the zipper run, do the buttons align.
Review the proto like an engineer, not a stylist. Measure every dimension against the spec chart and record the deviations. Wash it once if wash performance matters to your market — a proto that shrinks out of tolerance has just saved your program. Common proto findings include pocket depths that ignore mattress toppers, envelope closures cut too shallow, and pillowcase openings that gape. Each is trivial to fix now and miserable to fix in bulk. Approve the proto in writing, with your redlines marked on the spec chart, and the factory revises or moves on.
Stage Two: The Strike-Off, Locking Color and Print
While construction is being proven, color runs on a parallel track. For solid dyeing, the lab dip is a small swatch dyed to your Pantone TCX reference; for prints, the strike-off is your actual artwork printed on your actual base fabric. This is the moment your design stops being a screen image and becomes a textile, and it deserves your slowest, most careful review of the whole process.
Judge strike-offs under standard D65 lighting, never under office fluorescents or a phone screen. Compare against the numbered color standard, not against your memory of the design file. For prints, check the repeat size, the registration of overlapping colors, the sharpness of fine lines, and the hand feel after printing — heavy ink coverage can stiffen a fabric, and that matters for a sheet that touches skin. Plan for two to three rounds on a new design: the first calibrates, the second refines, the third signs off. Keep a sealed reference swatch of the final approval; bulk production will be judged against that swatch, and your memory of the color will drift within a week.
Stage Three: The Pre-Production Sample, the Sealed Reference
The PP sample — pre-production sample — is the most important sample you will ever approve, because it is the contract in physical form. It is made in the correct fabric, the correct approved color, with the correct construction, ट्रिमहरू, लेबलहरू, and packaging. It is the factory saying: this is exactly what your bulk order will look like. Your approval says: agreed, बनाउनु 5,000 of these.
Treat the PP approval as the legal event it is. Check it against the final tech pack revision line by line, not against the proto from two months ago — specifications evolve during development, and the PP must reflect the latest version of everything. Photograph it, seal it, and keep one sealed set yourself while the factory keeps the counter-seal. When bulk production starts, the factory’s in-line inspectors and your third-party inspector all judge against this sealed reference. A disciplined PP process is also where our “लक्षित मूल्यको सम्मान गर्नुहोस्” policy does its quiet work: you named one all-in price after reviewing other quotes, we answered make or no-make, and the PP sample proves the construction we promised at that price is the construction you receive.
Stage Four: Bulk Production and the First-Article Check
With the PP sealed, bulk production begins — but the first pieces off the line get special treatment. The first-article check pulls the earliest finished sets and compares them directly against the sealed PP sample before the line ramps to full speed. This catches setup errors: a machine threaded for the wrong stitch density, a cutting marker from the wrong size ratio, a packaging station using last season’s insert card.
After first-article approval, production runs under in-line inspection, with pieces pulled hourly and checked against the PP reference and the measurement chart. Nothing about this stage should surprise you if the earlier stages were done properly — bulk is execution, not discovery. If your factory treats bulk as the place to solve design problems, the development process failed upstream, and no amount of final inspection can fully recover it.
The Approval Discipline: Six Rules That Prevent Most Disputes
The stages only work if approvals are disciplined. These six rules separate professional programs from expensive arguments:
- Approve in writing, हरेक पटक. A verbal “looks good” on a video call is not an approval. Use a simple approval form or a reply email that names the sample, the revision, and the decision: approved, approved with comments, or rejected with reasons.
- One approver on your side. Samples reviewed by committee come back with contradictory comments. Designate one person whose approval counts, and let everyone else advise that person.
- Comment against the standard, not the feeling. “The blue feels off” cannot be manufactured to. “The blue is half a shade darker than Pantone 19-4052 TCX under D65” can be. Numbered standards turn taste into instruction.
- Freeze the spec at PP. After the PP sample is sealed, changes are change orders with cost and schedule impact, stated in writing before work continues. Late changes are the number-one cause of bulk surprises.
- Keep your own sealed references. Do not rely on the factory’s shelf alone. Your sealed proto, strike-off, and PP samples are your evidence if a shipment ever goes to dispute.
- Answer on schedule. Approval deadlines cut both ways. A factory holding greige and line time while waiting two weeks for your comments will either miss the ship date or rush the work. Put approval turnaround times in the development calendar and honor them.
Where Development Usually Goes Wrong
Three failure patterns cover most disasters. The first is the drifting tech pack: revisions discussed on calls but never consolidated into a new revision, so the factory builds to revision C while the buyer judges against revision E. The fix is dull and total — one controlled document, every change logged. The second is the unrepresentative sample: a proto approved in a substitute fabric that is then treated as approval of hand feel, or a strike-off approved on a different base cloth than bulk will use. The fix is labeling every sample with what it does and does not prove. The third is approval by silence: samples sit unanswered, production starts “to hold the schedule,” and the buyer later rejects goods built on an approval that never happened. The fix is the written-approval rule above, enforced without exceptions.
Notice what these three have in common: none of them is a manufacturing failure. They are communication failures wearing manufacturing costumes. The factories that deliver consistently are usually not the ones with the newest machines; they are the ones with the tightest paperwork. When you audit a manufacturer, ask to see a completed development file from a past program — the tech pack revisions, the sample approval forms, the sealed references. A factory that keeps immaculate development records will keep your program immaculate too.
Oem, Odem, and When the Factory Designs With You
Not every brand arrives with a finished tech pack, and a capable manufacturer should meet you where you are. In an OEM relationship, you supply the design and the factory executes it to your specification — the playbook above applies in full. In an ODM relationship, the factory contributes design: fabric suggestions, print directions, construction options drawn from what it already produces well. पूर्णता कपडा works both ways, developing across bedding sets, duvet and quilted sets, कपास र लिनेनदेखि बाँसको फाइबरसम्मका कपडाहरू, TENCEL lyocell र flannel, plus hotel linen, कम्बल, र तकियाहरू.
ODM does not mean skipping stages; it means the factory helps write the tech pack before the stages begin. The proto, strike-off, and PP discipline applies identically, because the physical approvals are what protect both sides regardless of who drew the sketch. If anything, ODM programs need the discipline more, since design intent lives in two organizations instead of one.
बारम्बार सोधिने प्रश्नहरू
What is the difference between a proto sample and a PP sample?
A proto proves the construction — measurements, seams, closures, fit — usually in a substitute fabric. A PP (पूर्व उत्पादन) sample is the finished article in the correct fabric, रंग, ट्रिमहरू, and packaging, and your approval of it authorizes bulk production. Think of the proto as the draft and the PP as the signed contract.
How many strike-off rounds should I budget for?
Plan for two to three rounds on a new design, at roughly one to two weeks per round including courier time. The first round calibrates color, the second refines it, the third is typically the sign-off. Complex multi-color prints or difficult shades may need an extra round; that is normal and far cheaper than correcting bulk.
Who pays for samples?
Practice varies: many factories charge development fees per sample that are credited against the bulk order once production is confirmed. Agree the terms in writing before development starts — fee per sample type, how many rounds are included, and what triggers a re-charge. For committed programs, sampling cost is a rounding error against the value of what it prevents.
Can I change the design after approving the PP sample?
You can, but it becomes a formal change order with stated cost and schedule impact, agreed in writing before work continues. This is why the spec freeze at PP matters: late changes ripple through fabric reservations, cutting markers, and line scheduling. Small tweaks are manageable; structural changes may mean re-sampling.
What should I do if bulk goods do not match the sealed PP sample?
Compare the goods against your own sealed reference under standard lighting, document every deviation with photos and measurements, and raise it through your merchandiser immediately — before the goods ship if possible. This is exactly why you keep sealed references and written approvals: they turn a disagreement about memory into a comparison of objects.
Start Your Next Program With the Paperwork Right
The brands that get consistent bulk production are not lucky; they are disciplined. One controlled tech pack, a proto that proves construction, a strike-off that locks color, a sealed PP sample that authorizes bulk, and written approvals at every step — that is the whole playbook, and it fits on one page. हामीलाई सम्पर्क गर्नुहोस् with your tech pack, even a rough one, and our merchandising team will turn it into a development plan with sample stages, approval deadlines, and one clear target price. हाम्रो अन्तर्गत “लक्षित मूल्यको सम्मान गर्नुहोस्” नीति, you name the price after reviewing your options and we answer make or no-make — then the samples prove we meant it. Alex@integritytex.com वा WhatsApp इमेल गर्नुहोस् +86 151 5289 1159.